
Towpreg and wet winding may produce the same geometry, but differ in when and how resin reaches the fibre, process control, speed, storage and investment.
Short answer
In wet winding, dry fibre passes through a resin bath on the winding line; towpreg is pre-impregnated at a controlled resin content. Select by volume, quality target and part geometry.
Why does it matter?
Resin content, fibre alignment, void fraction and winding speed directly affect repeatability in safety-critical products such as pressure vessels or shafts.
Key differences
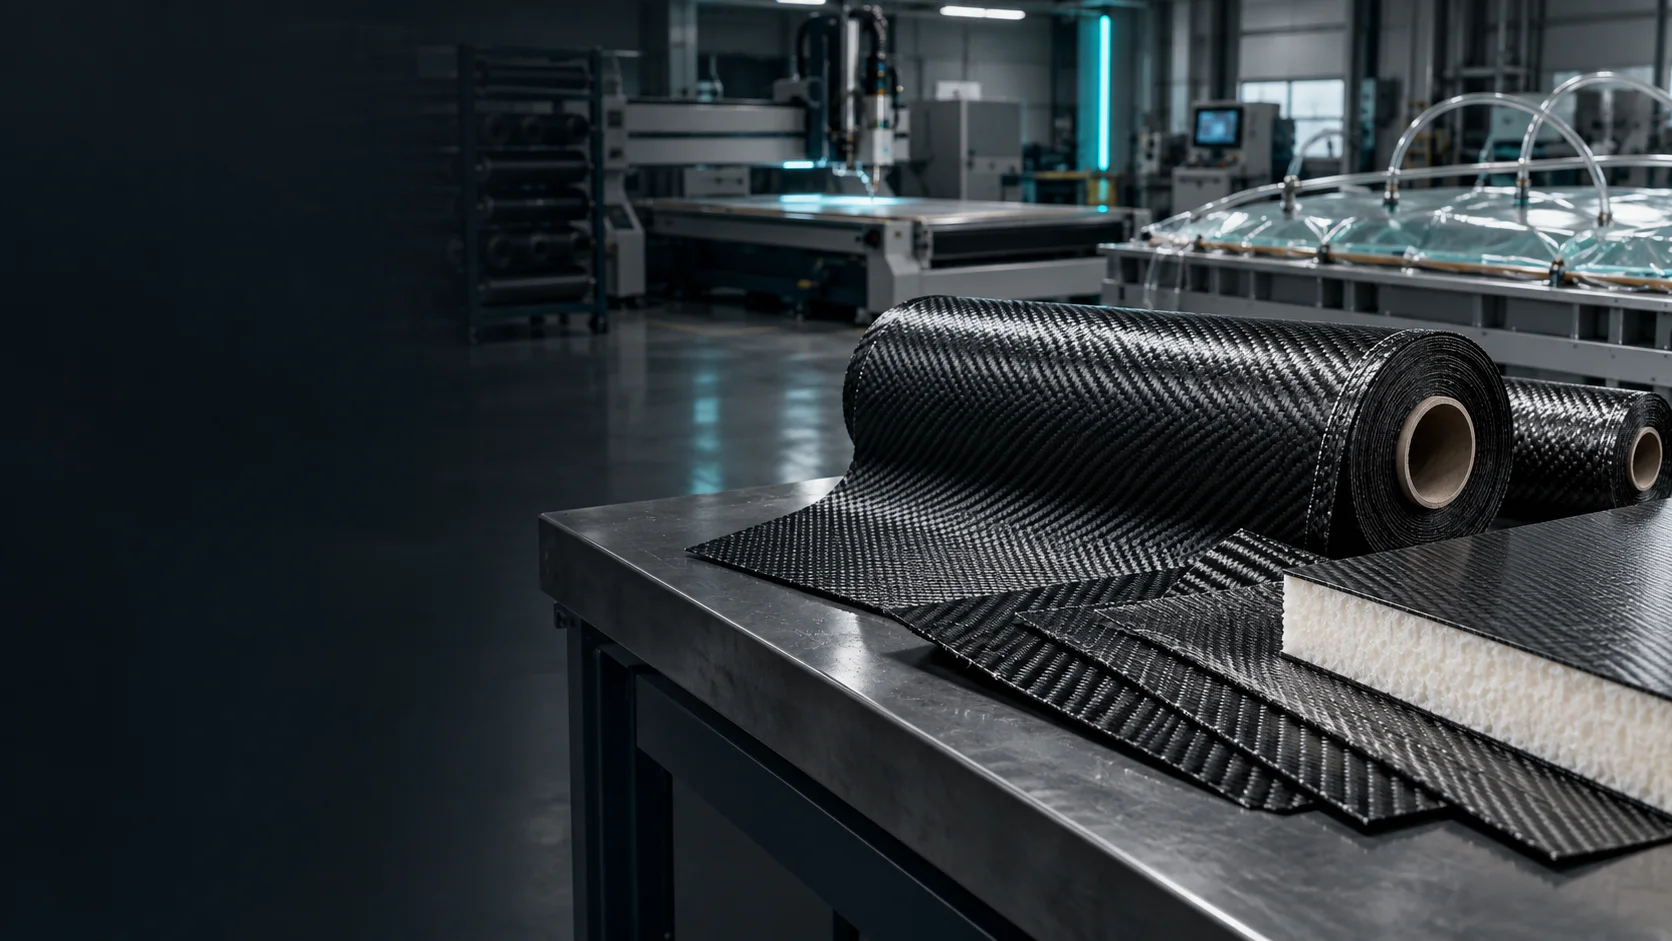
Wet winding can offer flexible resin choice and lower material cost; towpreg can improve resin-content control and shop cleanliness.
- Wet winding: resin bath, pot life and viscosity control
- Towpreg: cold storage/shelf life and prepreg quality control
- Both: winding angle, tension and cure-cycle validation
Selection matrix
Towpreg may lead in high-volume tight-tolerance production, while wet winding may suit development programmes with frequent resin changes. Decide on total process cost.
Frequently asked questions
Is towpreg always faster?
No. Storage, setup, cure and quality control determine the total cycle even if winding speed increases.
How is resin content controlled in wet winding?
Monitor bath temperature, viscosity, wipe geometry, fibre speed and tension together.
Conclusion and technical support
See our carbon-fibre supply guide for reinforcement architecture options.
Sources
- https://www.saertex.com/
- Üretici towpreg/reçine TDS belgeleri